Business
How Can Electronics Companies Manage Inventory Without Creating Excess Risk?

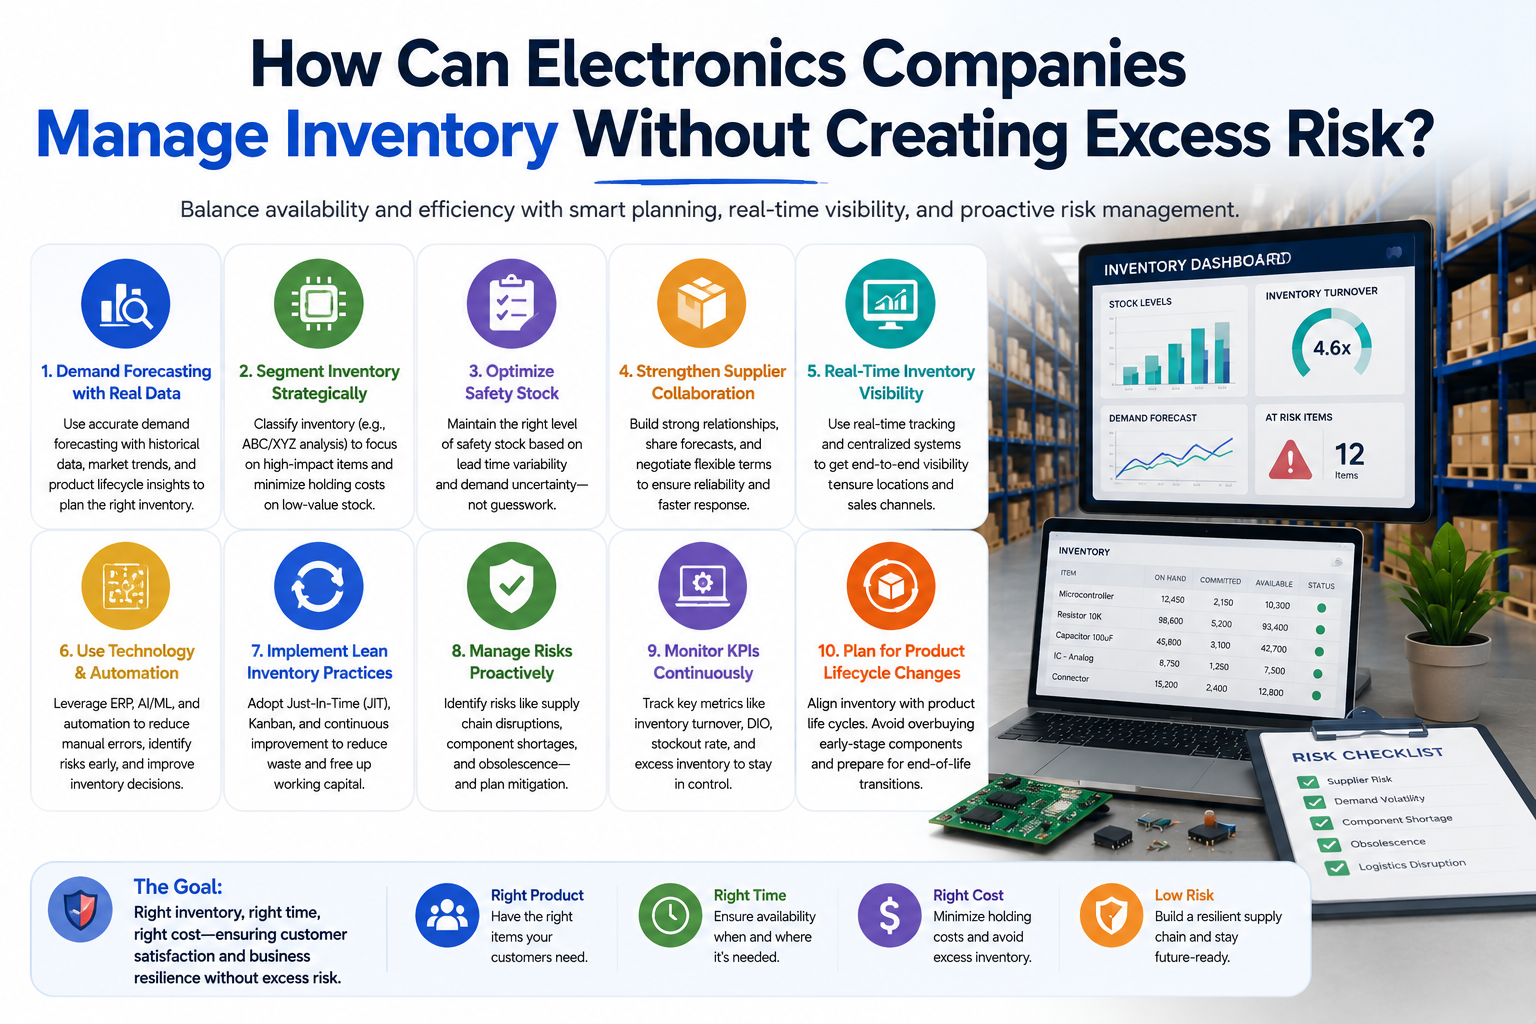
When I spoke last Spring with a procurement manager for a large manufacturing company, he had a storage room full of capacitors that he couldn’t use. He had purchased thousands of them 18 months prior, during the peak of the capacitor shortage, when the market rate was higher than normal. Today the market is no longer as tight and his budget has been slowly and quietly drained away while he waits for them to be used. He said that they “overcorrected” and I felt relief and sorrow for him that he did the right thing at the wrong time.
It’s such a clean word for such a messy problem. I kept thinking of people running for the train, but it has already left the platform. I’ve talked with many people in the industry and it doesn’t get any less painful.
The real tension nobody talks about honestly
In supply chain inventory management there are two games going on. Two games with two sets of rules and two penalties for losing each game. Most companies are playing the shortage protection game and, when that doesn’t work, they try to play the carrying cost control game using the rules of the other game. This fails.
Two games are being played. One for shortage protection. The other for managing the carrying costs of inventory. The rules for each game change constantly.
Once a company has once gone into “shortage mode” and then comes back to normal “carrying cost charged” type of inventory they have a hard time to switch back and forth between the two methods of managing their electronics inventory.
Why demand planning is harder than anyone admits
Everyone wants to improve their demand forecasting, but few realize just how difficult it is to forecast the demand for individual components required to produce a product. It is very difficult to forecast the demand for parts that are used in variable combinations in a variety of different products, with fluctuating customer orders, in a global market with fluctuating lead times, and in a market where the supply chain can collapse suddenly. And, yet, that is exactly what most companies are attempting to do. I get frustrated with procurement guides that treat demand planning for component inventory as if it were a solved problem that can be addressed with the right spreadsheet.
Real levers.
- Rolling forecasts updated monthly, not locked quarterly plans that become fiction by week six
- Tighter feedback loops between your sales team and procurement, so a shift in customer demand doesn’t take three weeks to reach the people actually placing orders
- Historical consumption data actively used in decisions, not just archived
- Explicit assumptions about lead time variability built in by component category, rather than treating everything as though it carries identical risk
Yes. No fancy conferences or keynotes required for that sort of work. It’s real machinery that works in really deep and subtle ways.
“Safety stock” — a living variable, not a fixed answer
A common way that inventory policy is framed out is as a number for safety stock to be calculated one time per year and then a wall to be hung in a meeting held annually. In reality a component with a 4-week lead time will have a vastly different required safety stock number than a component with a 26-week lead time. A part used in 12 different products will require a vastly different strategy for inventory management than a component used in a single SKU that will likely be cancelled in a quarter.
However, when developing a safety stock calculation, it is also reasonable to consider factors such as the supplier’s historical performance, the allocation of available supply to market demand versus stockpiled by suppliers, and whether the part in question is a single source item or if there are qualified alternate components for that part that are currently in inventory. Companies that really get to understand the risks in inventory management use what I would term a “tiered” safety stock policy – rather than a single number that is to be applied uniformly across a company’s entire product line. I already mentioned that one size does not fit all when it comes to human medicine – and that is even more the case for a complex component such as used in electronics. For electronics companies operating in genuinely complex supply chains, working with specialists in electronic component inventory management can provide the structural architecture to actually operationalize this kind of tiered approach, rather than spending two years trying to build it from scratch while the market moves underneath you.
Working with a seasoned expert in electronic component inventory management for companies operating in very complex supply chains can give you the “building” or architecture to operationalize a true tiered safety stock strategy as opposed to spending 2 years trying to create and implement a strategy as the market continues to change.
| Cost category | What drives it | Often underestimated? |
| Capital cost | Money tied up in inventory that can’t be deployed elsewhere | Yes, especially in low-rate environments |
| Obsolescence risk | Parts discontinued or superseded before use | Massively |
| Storage and handling | Physical space, climate control, ESD requirements | Somewhat |
| Insurance and shrinkage | Loss, damage, administrative overhead | Almost always |
Obsolescence of the worst kind is usually by surprise. One finds out that the parts for which one holds inventory are no longer being made by the manufacturer of these parts. In stock are 10,000 or so of these parts. All of them are expensive clutter. The focus of those involved in inventory planning for the production of electronics has always been on the shortage problems for the parts for which they are planning. These potential problems are ample to cause any person considerable anxiety. Obsolescence risk need not even be considered.
The capital cost line also deserves lots of attention. For a company running at very low margins, the holding cost of an item can equal a lot of lost revenue very quickly.
So what does balance actually look like?
It’s a negotiable process — every component is different.
In terms of practices for bringing your inventory strategy up to speed and working in today’s highly volatile market, the trick is to review your current inventory policy on a cycle that is more frequent than annually. The majority of companies use a set of practices for managing inventory which were designed for and are fit for purpose in a relatively stable market. The market has changed a lot in the last few years and it is time to review the facts from the last quarter to see how well your current practices are working. The review of your current practices for managing your running stock of components should include a review of your current safety stocks for each component and an assessment of the split between running stock that you are holding at higher than normal levels of inventory in order to act as a hedge against anticipated future higher than normal costs for said component against those where increased holding of inventory would result in higher than normal increased carrying costs. Also, in reviewing your current safety stock for each component, you will undoubtedly find some where prior miscalculations have resulted in you currently holding levels of inventory that are higher than desired. It is essential that any re-design of your subsequent running stock safety stock is completed in a timely manner, but that the re-design is completed in a manner that does not give the impression that you are waffling or are afraid of your own decisions. The procurement manager in the earlier scenario redesigned his buffer stock methodology after his experience with the capacitors and, although not perfect, he is now slower to stockpile and far more selective in terms of the types of components that he feels merit a panic buy.
This brings me back to the original procurement manager shown with cases of capacitors. His “correction” to building buffer stock is much slower and much more deliberate then before. He only adds to stock when he intends to. No more panic buying! His new view of how to run his group of procurement inventory specialists is not perfect. But it’s in the right direction.

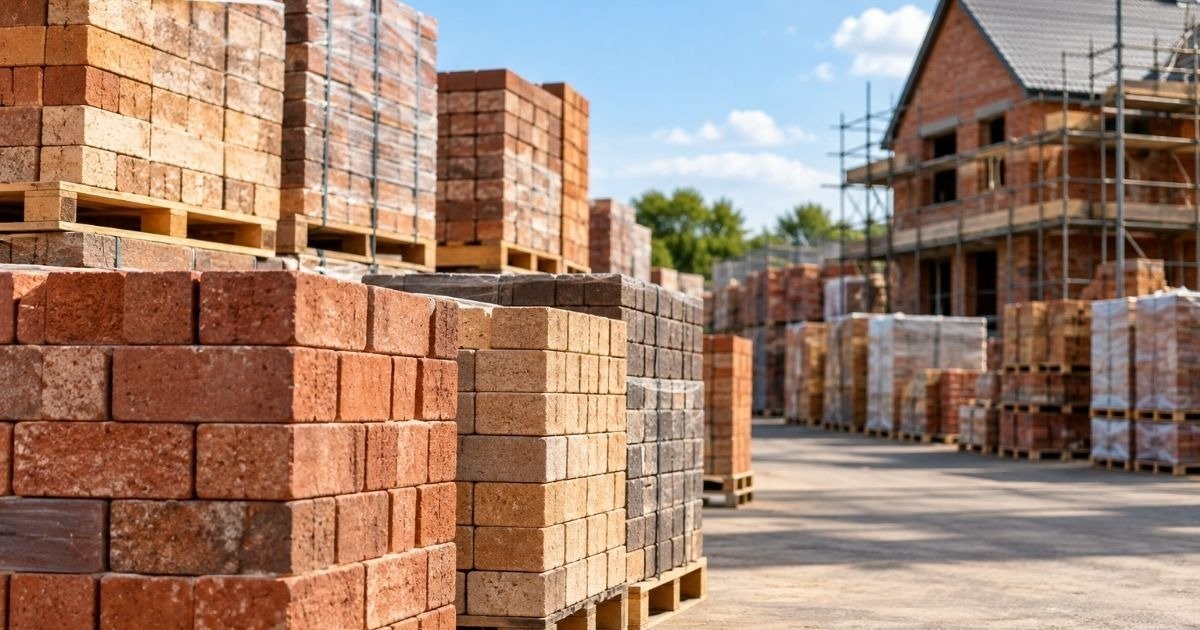
European clay bricks give UK architects access to colours, textures and formats that domestic kilns do not always produce. Danish, Belgian, Dutch and German manufacturers fire a wide range of facing bricks, from long linear formats to hand-thrown blends, and many have built strong reputations on award-winning UK schemes.
Importing them adds steps that a standard UK order never involves. Specifiers need to confirm compliance with British standards, buyers need to plan around freight and production slots, and contractors need a reliable route for samples, top-ups and after-sales support. Getting each stage right keeps the facade on budget and on programme.
How to Source European Bricks Step by Step
Here’s how to take an imported brick from first sample to final delivery on site:
1. Define the Look Before Contacting Suppliers
Start with a clear brief for colour, texture, format and bond. European ranges are broad, and a vague request tends to produce a long list of samples that slows the design team down. Pin down the face size, the mortar colour you have in mind and the finish you want across the elevation.
Texture is often the deciding factor. A smooth wirecut face reads very differently from pinhole bricks, where small surface perforations catch the light and add depth to a large wall. Agreeing these details early gives every supplier a firm target to match.
2. Match the Clay Type to the Colour You Need
A brick’s colour comes largely from its raw clay and the way it is fired. Iron-rich clays tend to fire to reds and browns, while the lime-rich clays found across parts of Belgium, the Netherlands and Denmark fire to paler yellow and cream tones.
If the design calls for a golden buff brick, focus your search on producers working with those lighter clays. Ask each manufacturer for photos of completed buildings and a sample panel, since a single loose brick rarely shows how colour shifts across a full elevation.
3. Benchmark Samples Against Familiar UK Bricks
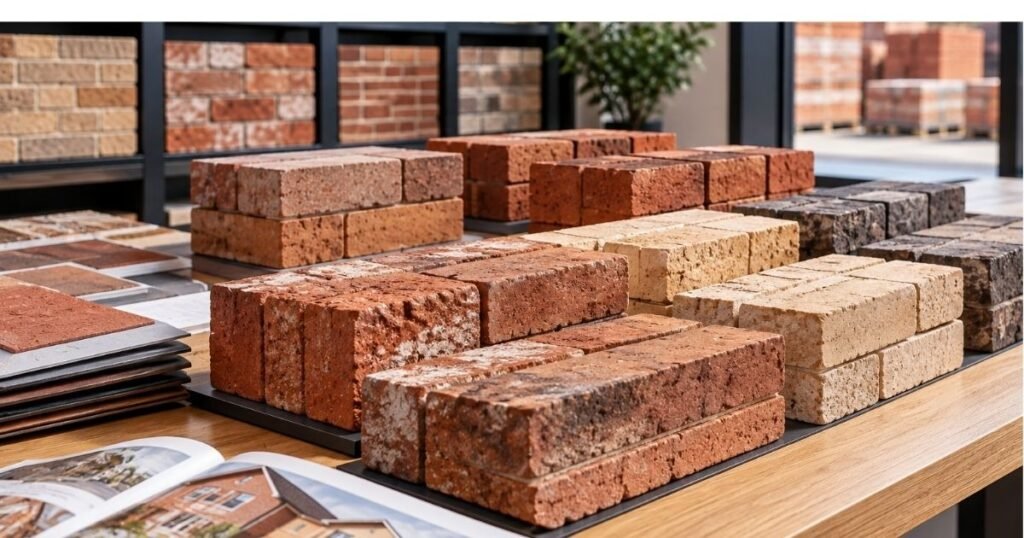
Planning officers and clients often judge new brickwork against bricks they already know. Where a scheme sits beside existing buildings, the approved palette may reference a domestic product, and any imported option has to sit within that range.
A common reference point is the Ibstock Alnwick Blend, a UK facing brick many design teams already recognise. Lay European samples beside a benchmark like this in the same light and the same mortar. It makes tone, texture and size differences easy to judge before materials go in for planning approval.
4. Check Standards and Compliance Paperwork
Clay bricks sold in Great Britain should be made to BS EN 771-1 and supplied with a Declaration of Performance. Confirm the product carries the conformity marking accepted at the time of purchase, and that its declared values suit the exposure of your site.
Pay close attention to these declared values, especially on exposed elevations, parapets and chimneys:
- Frost resistance: look for an F2 rating where brickwork faces severe exposure.
- Active soluble salts: an S2 category lowers the risk of sulfate attack on mortar.
- Water absorption: this affects mortar choice and how the wall weathers over time.
- Dimensional tolerance: tighter tolerances give cleaner joints on linear formats.
Review these figures with your architect or engineer, because responsibility for the final specification sits with the appointed designers and contractor under the Building Safety Act 2022.
5. Build Lead Times Into the Programme
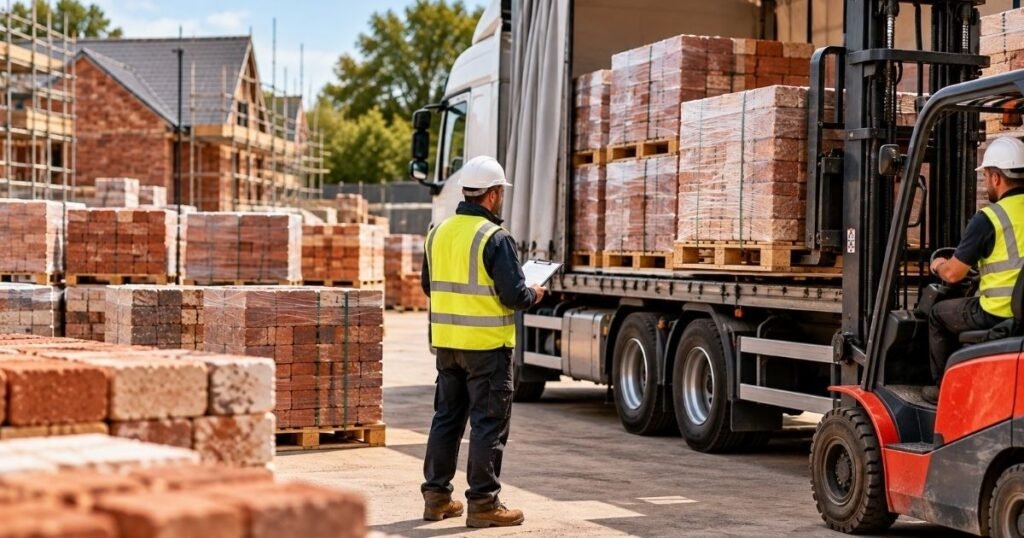
Imported bricks travel further, and production slots at popular European kilns are often booked well ahead. Allow time for manufacturing, freight, customs clearance and delivery to site, and agree call-off dates in writing with your supplier.
Order the full quantity from a single production run where possible. Clay varies between batches, and topping up from a later firing can leave a visible band in the brickwork. A small surplus held in storage costs far less than rebuilding a mismatched elevation.
6. Work With a UK Stockist That Imports Direct
Buying through an established UK importer removes a lot of the risk. A good stockist handles shipping, customs and paperwork, keeps samples ready for quick comparison and can arrange sample panels on site.
Local support also counts after delivery. If a pallet arrives damaged or the order falls short, a UK partner can resolve it far faster than a manufacturer overseas. Ask about storage, return terms and technical help before you place the order.
Bringing European Brick to Your Next UK Project
Sourcing European bricks starts with a clear design brief and ends with a well-planned delivery. Define the colour, texture and format first, then match the clay type to the tone you want. Benchmark every sample against familiar UK bricks so planners and clients can judge it with confidence.
Check the Declaration of Performance and declared values against the exposure of your site, and lock in production slots early to protect the programme. Ordering the full quantity from a single batch keeps the brickwork consistent. A trusted UK importer ties each stage together and keeps the facade looking right from the first course to the last.

Macroeconomic Drivers and Line Efficiency Trends in Modern Packaging
The global Food and Beverage (F&B) industry in 2026 operates under intense macroeconomic pressure. Chronic labor shortages across manufacturing hubs, volatile raw material prices, and accelerating consumer demand for packaged goods have forced plant managers to re-evaluate traditional packaging line workflows. Achieving high Overall Equipment Effectiveness (OEE) is no longer merely an operational objective; it is essential to protecting profit margins and meeting stringent output quotas.
Addressing Bottlenecks in Legacy Filling and Sealing Operations
Legacy packaging lines heavily reliant on manual handling or semi-automated mechanical drives create severe operational friction. Common failure points include:
- Throughput Speed Limits: Fixed mechanical linkages prevent dynamic speed adjustments during high-volume production runs.
- Volumetric Inconsistency: Manual and mechanical dosing mechanisms suffer from thermal expansion and wear, leading to product giveaway or under-filling.
- Sealing Integrity Risks: Inconsistent seam formation in manual or semi-automated sealing exposes sensitive F&B products to atmospheric oxygen, accelerating spoil rates and causing premature degradation.
Integration of Smart Servomotors and Automated Controls
Modern facilities are eliminating these mechanical bottlenecks by deploying integrated, multi-axis servomotor control systems managed by central programmable logic controllers (PLC systems). Independent servo-driven stations enable microsecond-level synchronization across the line, drastically reducing mechanical wear and mechanical vibration.
As consumer demand for eco-friendly and efficiently sealed canned products surges, leading packaging line manufacturers such as Levapack are providing customized automated canning and seam sealing solutions that help medium to large-scale producers significantly streamline their production lines.
By replacing rigid mechanical line shafts with adaptive digital drive controls, beverage and food processors achieve faster line balancing, automated recipe changeovers, and negligible container jam rates.
Technical Standards & Precision Engineering in Can Packaging
Packaging diverse F&B formulations—ranging from carbonated beverages and liquid sauces to hygroscopic powders and solid snacks—demands advanced mechanical engineering to safeguard product freshness and extend shelf life.
Vacuum Seaming and Atmospheric Nitrogen Gas Flushing
Preserving nutritional value and extending shelf life without artificial preservatives depends heavily on modified atmosphere packaging. Modern automated seamers integrate high-vacuum evacuation chambers alongside automated nitrogen gas flushing () manifolds.
This multi-stage process removes ambient air and reduces internal headspace oxygen below 0.5%. Lowering residual oxygen prevents lipid oxidation, preserves flavor profiles, and prevents package collapse during shipping across variable altitudes.
Modular Line Configurations: From Cleaning to Labeling
Modern packaging architectures utilize modular rotary and linear motion configurations that connect all stages of the packaging workflow into a seamless unit.
| Key Performance Metric | Traditional Mechanical Lines | Smart Servo-Driven Automated Lines |
| Throughput Speed (CPM) | Low-to-Moderate (40–80 cpm) | High-Speed (150–350+ cpm) |
| Sealing Defect Rate (%) | Higher (1.0% – 2.5%) | Minimal (< 0.05% via servo monitoring) |
| Changeover Downtime | Manual Tooling (2–4 hours) | Automated Recipes (< 15 minutes) |
| Maintenance & Downtime | Frequent reactive maintenance | Predictive diagnostics & low mechanical wear |
These modular systems connect linear container sterilization units with high-speed rotary seamers, checkweighers, and vision-guided labeling stations to minimize physical contact and maximize hygiene.
Safety, Quality Standards, and Equipment Reliability
Maintaining high-speed throughput must be balanced with strict food safety regulations and international equipment engineering standards.
Regulatory Compliance and Quality Management
Global food manufacturing demands complete traceability and verifiable quality systems. Facilities must ensure that automated machinery suppliers adhere to global standards such as the ISO 9001 Quality Management System, which establishes documented process controls, audited component sourcing, and rigorous quality benchmarks across automated assembly setups.
Furthermore, international machinery safety certifications—including CE marking for European compliance and CSA certification for North American electrical safety—verify that high-voltage drive electronics and pneumatic systems meet strict operator safety requirements.
Predictive Maintenance and Torque Safety Controls
Unplanned downtime on high-speed packaging lines can cost manufacturers thousands of dollars per hour. Modern automated seamers feature active torque control and overload sensors that continuously monitor motor feedback. If a jammed can or misaligned lid causes a sudden resistance surge, the system instantly triggers an automated safety stop to protect vital drive mechanisms and reduce material scrap.

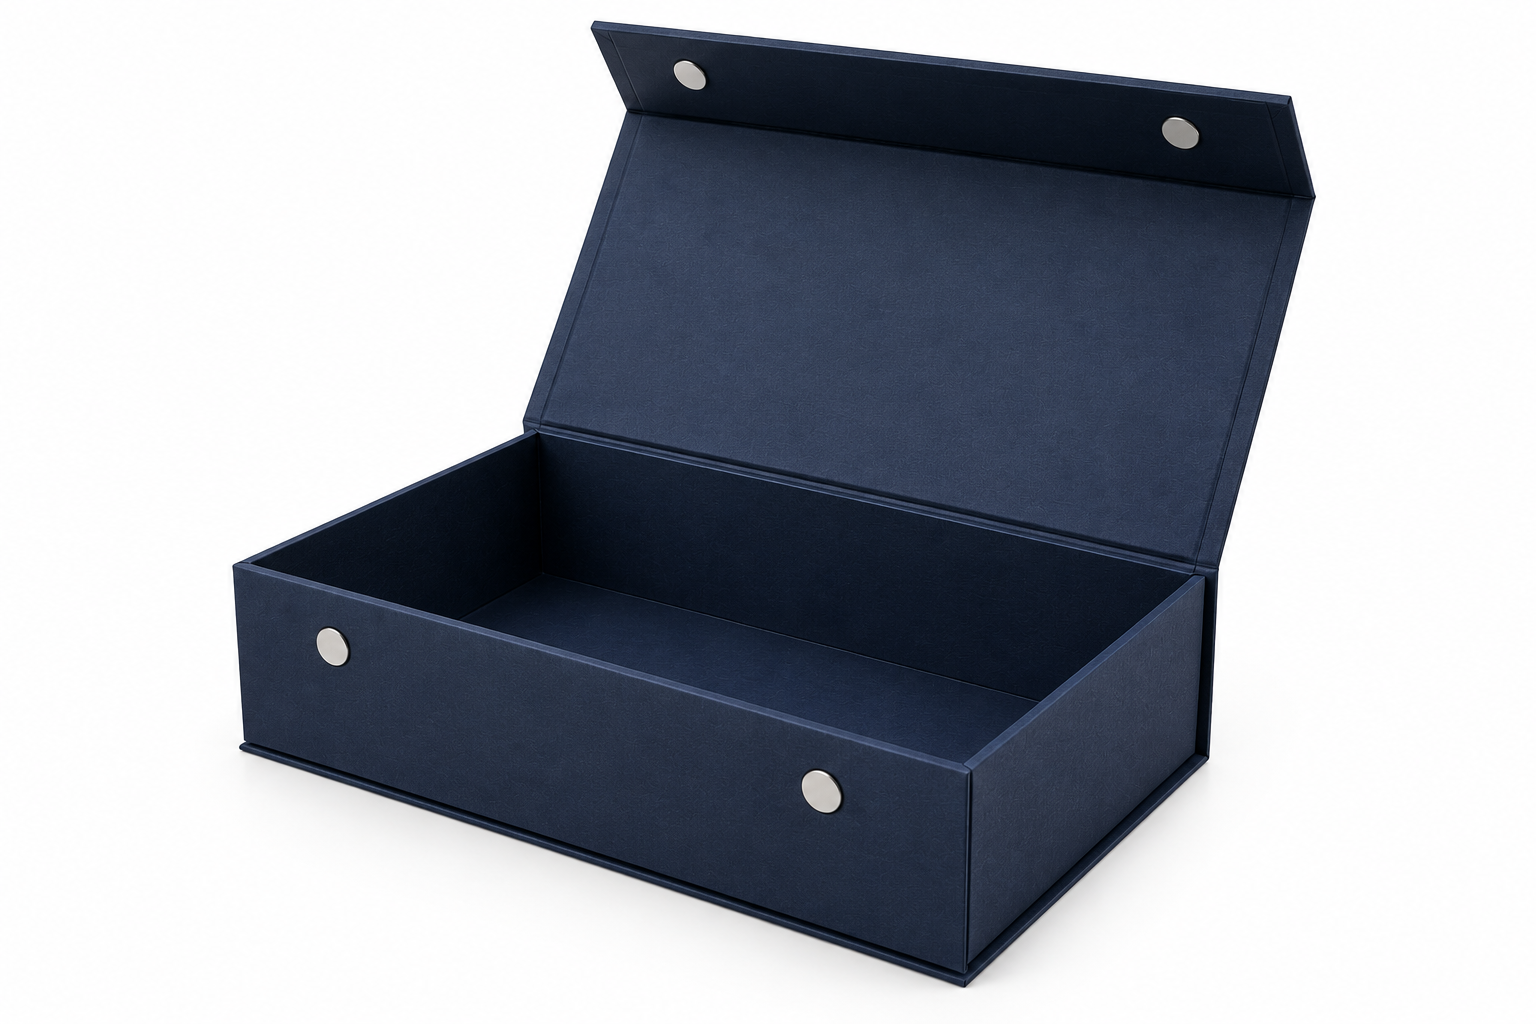
Hunting and researching new ways to increase customer loyalty is a standard practice for brands that want to increase their influence in the market. Spending heavily on marketing to acquire new buyers is one thing but keeping them coming back to your brand is something that is much harder. What if we tell you a way with which you can increase your repeat purchase rate by 35%?. And that too simply by upgrading your packaging style? Custom magnetic rigid boxes are one of the most powerful proven solutions. That can transform a standard unboxing experience into something that is highly memorable and feel-worthy.
Your customers will come back eagerly for more. Since they will remember the premium feel that they felt when they held your products in their hands. Let us tell you exactly how custom magnetic boxes can drive this incredible retention rate.
The Psychology of the Unboxing Experience
The review of your customers about your brand and its products begins to form within seconds after they receive or buy something from your site. If they have a flimsy cardboard in hand, it’ll send them a direct message of cheapness. On the other hand luxury magnetic boxes will make them feel high value and prestige the moment they set eyes on them. They simply cannot avoid the dopamine rush that they feel with the smooth slide of your box’s lid. And the satisfying snap of its magnet.
This experience triggers a deeply positive emotional attachment with your product. As a consequence if your customers feel good, they will associate that happiness and joy directly with your brand. Magnetic closure packaging instantly uplifts the value of whatever it holds inside of it. The buyers feel that they have something truly special in hand and this can surely make them excited to make a repurchase.
Durability Encourages Reusability
What happens to standard cardboard boxes is that they get thrown away immediately after unboxing. People tend to retain strong beautiful packaging since they feel that they can use it for a different purpose later on.
Magnetic packaging boxes are flawless when it comes to the shipping process. Their strong construction protects the product that is inside of them perfectly. After the customer takes out the product, it is very rare that they trash the box. Instead they use it to store other items or important keepsakes. This simple action can turn your packaging into a long-lasting piece of home decor.
Your brand name comes into the picture every time the customer opens or reuses the box. Printed magnetic closure boxes keep your logo and your branding visibly present in their homes for months or even years. This constant yet subtle reminder of your brand’s existence can drive repeat sales organically.
Customization Amplifies Brand Identity
You simply have to take out generic packaging from your options if you want to make your brand stand out on the shelf and in the customer’s mind. You can design custom magnetic boxes to mirror your brand identity in a perfect way. The choice of colors, the interior lining, and the exact placement of your logo, create a unified brand experience. Your buyers will definitely notice the careful attention to detail and they will trust your brand even more deeply. Customer trust directly translates into a higher repeat purchase rate.
Igniting Social Sharing and Word of Mouth
Social media is all about the exciting experiences that people want to share and make others know about. If you look closely, a simple box rarely makes its way onto social media platforms. On the other hand, luxury magnetized boxes almost beg to be filmed. Their buyers record the whole experience that they have with the box. Including the satisfying snap of the magnet, and post unboxing videos for their followers.
This organically generated content acts as free but highly effective advertising for your brand. Every person who watches such types of videos wants to have the same experience. As a result they visit the store and buy the same product. This way your existing customers become your best marketers. Magnetic closure packaging directly fuels this viral and most profitable marketing loop.
How Exactly Does This Drive a 35% Increase?
This thought concerns many people: how a simple Changing the switch can change the buying behavior so drastically. Here is a breakdown of how custom magnetic closure boxes manage to deliver these impressive numbers.
- Enhanced assumed value : Customers begin to feel that they got more for their money when they hold a magnetic box in their hand. This higher value justifies premium price points.
- Memorable interaction: The magnetic snap tends to stick to memory, which builds up sensory marketing. Sensory marketing is known to make stronger emotional connections than visual marketing alone.
- Home retention: If you manage to create boxes that are reusable, you will make your brand visible indefinitely. In the modern market out of sight means out of mind. Reusable boxes protect your brand from becoming invisible.
- Gift-ready beautification : Customers love it when they get packaging that is beautiful enough to be given out as a gift. This initiates repeat purchases because the packaging makes gifting a little easier.
The power of premium packaging is not something that you can afford to ignore anymore. The upgrade of your packaging strategy can solve your retention problems in the most efficient way. If you invest in luxury rigid boxes, you create an unboxing experience that your customers will actively crave. This positivity guarantees that they will choose your brand over and over again. Start designing your magnetic boxes today and watch your repeat purchase rate climb.
.

The Conflicts Nobody Thinks To Declare

How to Source European Bricks for UK Building Projects

How Automation is Reshaping the Global Food & Beverage Packaging Industry in 2026
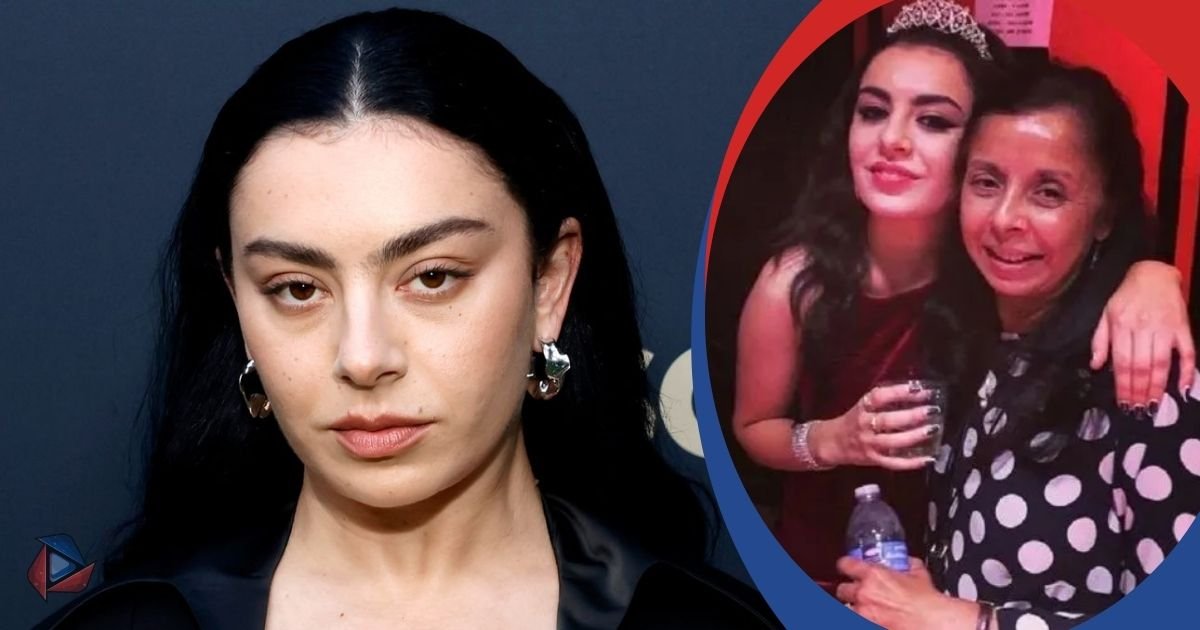
Who Is Shameera? All You Need To Know About Charli XCX’s Mother
Who Is Gulliver Flynn Oldman? The Untold Story of Sir Gary Oldman’s Son
Meet Rosemary Turner: The Mother of Actor Callum Turner
-
Biographies8 months ago
Who Is Shameera? All You Need To Know About Charli XCX’s Mother
-
Biographies8 months ago
Who Is Gulliver Flynn Oldman? The Untold Story of Sir Gary Oldman’s Son
-
Biographies8 months ago
Meet Rosemary Turner: The Mother of Actor Callum Turner
-
 Biographies6 months ago
Who is Alexandra James? Inside The Life of Jeremy Clarkson’s Former Partner
-
 Biographies8 months ago
Who is Todd McRae? Meet Tate McRae’s Father
-
 Biographies7 months ago
Who Is Daniel Mara? The Untold Story of Kate Mara’s Private Sibling
-
 Celebrity8 months ago
Who Is Peter Hernandez? The Real Story of Bruno Mars’ Father
-
 Biographies8 months ago
Who Was Adrian Mayers? The Untold Life of A$AP Rocky’s Late Father